



Private Label vs OEM Coffee Capsules: What’s the Practical Difference
A buyer says they need private label coffee capsules. Another asks for OEM. A third uses both terms in the same email to describe exactly
A factory tour can be impressive without telling you very much.
You see machines running. Finished capsules are neatly arranged. Someone explains the production line, shows a few inspection instruments, and takes you through a clean warehouse.
All useful.
But none of it, by itself, answers the question a professional buyer actually needs answered:
“Can this factory repeatedly manufacture the product we’ve approved?”
That’s what a useful factory audit should establish.
For coffee capsule buyers, an audit isn’t really about finding the newest machine or the largest building. It’s about connecting what a supplier says it can do with evidence of how production actually works.
How is material identified when it arrives?
How does an approved product specification reach the production floor?
Which characteristics are controlled while capsules are being made?
What happens when something goes wrong?
Can a complaint be traced to a production lot?
And is the manufacturer’s claimed output realistic once quality inspection, finishing and packaging are included?
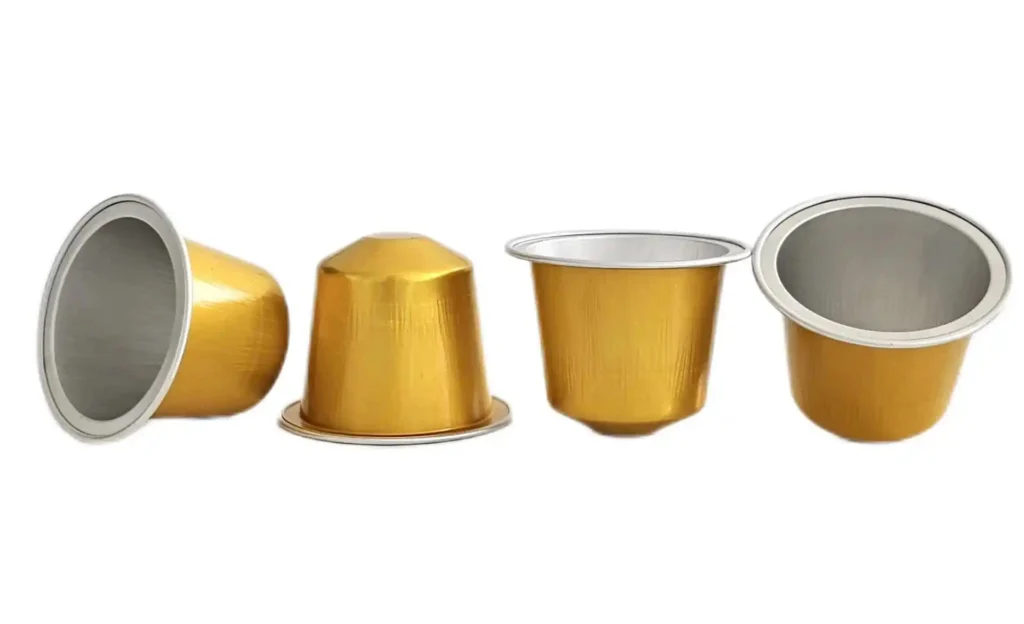
When evaluating an empty aluminum coffee capsule manufacturer, these questions usually tell you more than a showroom ever will.
A useful audit begins before the factory visit.
If the buyer hasn’t defined what needs to be verified, the visit can easily become a guided tour rather than an audit.
Start with the project.
Which capsule are you planning to buy?
What volumes do you realistically expect?
Does the project involve standard products or customization?
Will the capsules run on automated filling equipment?
Which technical, food-contact or commercial documents matter to your organization?
Once those requirements are clear, the audit can focus on whether the factory has the systems needed to support them.
This is also why a broader coffee capsule supplier qualification process shouldn’t depend on the site visit alone. Samples, technical documentation, communication, commercial capability and actual manufacturing evidence all contribute to the qualification decision.
A factory audit is one piece of evidence.
An important one, but still one piece.
Most factory visits have a route prepared in advance.
A more revealing way to understand manufacturing is to mentally follow the product instead.
Start where materials enter.
How are incoming materials identified?
Can the factory distinguish different material lots?
Where are they stored?
What prevents an incorrect material from being released into production?
How is the material linked to the product eventually manufactured from it?
For food-contact packaging, also ask which documentation relates to the material or finished food-contact construction and whether that documentation applies to the actual product you’re purchasing.
You don’t necessarily need to inspect every warehouse record yourself.
The point is to see whether a logical chain exists from incoming material to finished product.
If the factory cannot explain that chain clearly, later traceability becomes much harder.
Equipment is probably the easiest thing to notice during an audit.
Don’t stop at counting machines.
Ask what each critical operation actually controls.
For capsule forming, for example, the useful discussion isn’t only about machine speed. It’s about whether the process can repeatedly create the geometry required by the approved specification.
Look at how equipment is set up.
How are different products or specifications changed over?
How are settings controlled?
What happens after maintenance or tooling changes?
How is production checked after the line restarts?
A highly automated machine can improve consistency, but automation itself doesn’t prove process control.
The factory still needs to know what acceptable output looks like and how it will recognize when production begins moving away from that target.
Machines create output.
Process control makes that output useful.
A buyer approves a sample and technical specification.
Then what?
This question is surprisingly important.
The approved product needs to be translated into information the production and quality teams can actually use.
Which drawing or specification is current?
How is the correct color or finish identified?
Which artwork version applies?
If the lid or packaging is part of the order, how are those requirements linked to the job?
How does the production team know they’re working from the latest version rather than an obsolete one?
This is basic version control.
It doesn’t need to involve sophisticated software.
A simple system that is consistently followed is much more valuable than an expensive system people routinely bypass.
During an audit, ask for an example of how a production order moves from commercial approval into manufacturing. Sensitive customer information can be hidden; you’re looking at the process, not another buyer’s confidential data.
A room full of measuring equipment can look reassuring.
The more useful question is how those measurements influence production.
Which characteristics are inspected?
Which are checked during production and which at final inspection?
How are results recorded?
What happens if a measurement is approaching—or has moved outside—the agreed requirement?
Who has authority to stop or adjust production?
How are affected products identified?
These questions tell buyers whether quality control is integrated into manufacturing or exists mainly as an inspection function at the end.
A useful coffee capsule quality control process should do more than find defective pieces.
It should provide information about whether the manufacturing process remains stable.
During an audit, a buyer doesn’t necessarily need to see confidential customer records. An anonymized example of an inspection record or quality workflow can still demonstrate how the system operates.
Traceability can feel unnecessary when every delivery is perfect.
Its value appears when one isn’t.
Suppose a customer reports leakage in part of a shipment.
Can the supplier identify which production lot the capsules came from?
Can they connect that lot to relevant production and inspection information?
Can affected inventory be separated from unaffected inventory?
Can the manufacturer determine whether the issue is isolated or potentially broader?
Traceability doesn’t automatically solve the technical problem.
It reduces uncertainty around it.
This is particularly important for repeat orders because otherwise the investigation can quickly become guesswork:
Was it the latest batch?
An older shipment?
A different lid?
A different production setup?
Good traceability gives the investigation somewhere to start.
Capacity is one of the most common numbers buyers ask for.
It’s also one of the easiest numbers to misunderstand.
A machine’s theoretical maximum output isn’t necessarily the factory’s sustainable commercial capacity.
Real production includes setup, product changes, maintenance, quality checks, finishing, packaging and other constraints. Different SKUs may also consume capacity differently.
Instead of asking only:
“How many capsules can you produce per day?”
Ask:
What equipment or production lines support that figure?
Is it theoretical or based on actual production?
What are the main bottlenecks?
Can finishing and packaging handle the same output?
What happens when several customer orders overlap?
How much capacity is realistically available for a new customer?
Evaluating coffee capsule production capacity this way gives procurement teams a much more useful picture of supply capability.
A large number is easy to print in a brochure.
Reliable output is harder to fake during a serious audit.
Warehouses are easy to treat as the least technical part of a factory tour.
They shouldn’t be.
Look at how materials and finished products are identified.
Are lots separated clearly?
How are products protected from unnecessary damage?
Are cartons stored in a way that avoids excessive compression?
Can the warehouse team identify which finished goods belong to which production order?
For empty aluminum capsules, physical protection matters because damage to the rim or body geometry can create problems later on a filling line.
A capsule can pass final inspection and still become unsuitable if it is poorly handled afterward.
The warehouse is therefore not where quality control ends.
It’s where preservation of the finished product begins.
Perfect factories don’t exist.
An audit becomes much more informative when a supplier is willing to explain what happens when production doesn’t go perfectly.
How is non-conforming product identified?
Is it physically separated?
Who decides whether it can be reworked, reclassified or must be rejected?
How is the decision recorded?
If an issue repeats, is there a process for investigating the cause?
Buyers sometimes feel reassured when a supplier claims:
“We never have defects.”
That answer should usually create more questions, not fewer.
Manufacturing variation exists.
The sign of a mature quality system isn’t the claim that problems never happen.
It’s the ability to identify, contain, investigate and learn from them.
Factory audits are most useful when buyers ask to understand a process rather than simply confirm a checklist.
“Do you have quality control?”
The answer will almost always be yes.
“How does a dimensional problem discovered during production affect the rest of that production lot?”
That’s a much better question.
The same applies to capacity, traceability and material control.
After more than 10 years in aluminum coffee capsule manufacturing, we’ve found that buyers get a clearer picture of a factory when they follow a few real scenarios from beginning to end.
Show me how this material becomes this product.
Show me how this specification reaches the machine.
Show me what happens when a measurement fails.
Show me how this carton can be traced back to production.
Those conversations reveal the manufacturing system behind the equipment.
And that’s what a factory audit is really there to verify.
When the audit is over, try to separate what you saw from what you verified.
You may have seen impressive equipment.
What evidence showed that it produces your required capsule consistently?
You may have seen inspection instruments.
What evidence showed how they’re used during production?
You may have seen a large warehouse.
What evidence showed that lots are identified and protected properly?
You may have heard a large capacity number.
What evidence supported it?
That’s the difference between touring a factory and auditing one.
A good audit doesn’t need to make the supplier look perfect.
It should make the manufacturing system understandable.
When procurement teams can see how material, production, quality, traceability, capacity and warehousing connect, they’re in a much stronger position to decide whether a factory can support commercial production—not just a successful first order.
Ofte stilte spørsmål
Should buyers always visit a coffee capsule factory in person?
Not necessarily. An on-site audit can provide strong evidence, but remote factory reviews, live video tours, documentation, samples and third-party audits can also contribute to supplier qualification when travel isn’t practical.
What is the most important thing to check during a factory audit?
There isn’t one universal item. The most useful goal is to verify that the factory has a controlled process capable of repeatedly producing the product you intend to buy. Material control, manufacturing, quality, traceability and capacity all contribute to that conclusion.
How can buyers verify a manufacturer’s production capacity?
Ask what equipment and production lines support the stated capacity, whether the figure is theoretical or based on actual output, what the manufacturing bottlenecks are, and whether quality inspection, finishing and packaging can support the same volume.
Why should buyers check traceability?
Traceability helps identify which production lot is involved when a quality issue occurs and can connect finished products with relevant production and inspection information. This makes problem investigation and containment more effective.
Is having ISO or other certificates enough to qualify a capsule factory?
No. Relevant certifications can be useful evidence, but they don’t replace product testing, process evaluation, manufacturing evidence, documentation review and confirmation that the supplier can meet the requirements of your specific project.
Spesialist innen produksjon av kaffekapsler · Kervoo
Siden 2024
A buyer says they need private label coffee capsules. Another asks for OEM. A third uses both terms in the same email to describe exactly
A perfect sample is reassuring. It looks right. The color is right. It drops into the machine smoothly and brews without leaking. Put ten more

En god presentasjon er ikke det samme som gode bevis. Leverandørens nettside, katalog og salgspresentasjon er nyttige utgangspunkt. De kan gi deg informasjon om