

Private Label vs OEM Coffee Capsules: What’s the Practical Difference
A buyer says they need private label coffee capsules. Another asks for OEM. A third uses both terms in the same email to describe exactly
A larger coffee capsule order will usually give you a better unit cost.
That doesn’t automatically make it a better order.
If six months of capsules arrive for a product that only sells through in twelve months, the purchasing team may have improved the unit price while making inventory worse. Add several colors, slow-moving SKUs and international freight, and that “good deal” can tie up considerably more cash than expected.
The opposite creates its own problem.
Order too cautiously, and the next production run may not arrive before existing inventory is exhausted.
For buyers planning wholesale or bulk purchases of empty aluminum coffee capsules, the useful question is therefore not:
“How many can we buy?”
It’s:
“How much should we buy now, and when will we realistically need the next order?”
The answer comes from several numbers working together: actual demand, SKU mix, MOQ, usable inventory, supplier lead time, international transit and the amount of uncertainty your business can tolerate.
Supplier quotations often encourage buyers to think in quantity tiers.
20,000 pieces cost one amount per unit. At 100,000, the unit price may improve. Go higher and production economics may improve again.
That’s useful information.
But it isn’t demand.
Before deciding order quantity, estimate how quickly the business actually consumes capsules.
For an existing product, historical usage is the strongest starting point. Look at several months rather than one unusually strong period. If demand is seasonal, compare like-for-like periods where possible.
For a new product, the estimate will naturally be less certain. In that case, it’s usually better to work with scenarios rather than pretend the forecast is precise.
Par exemple :
Expected case: 20,000 capsules per month
Lower-demand case: 12,000 per month
Higher-demand case: 30,000 per month
These figures are examples, not industry benchmarks. Their purpose is to show what happens to inventory under different sales conditions.
If a 100,000-piece order looks comfortable only in the highest-demand scenario, the order deserves another look.
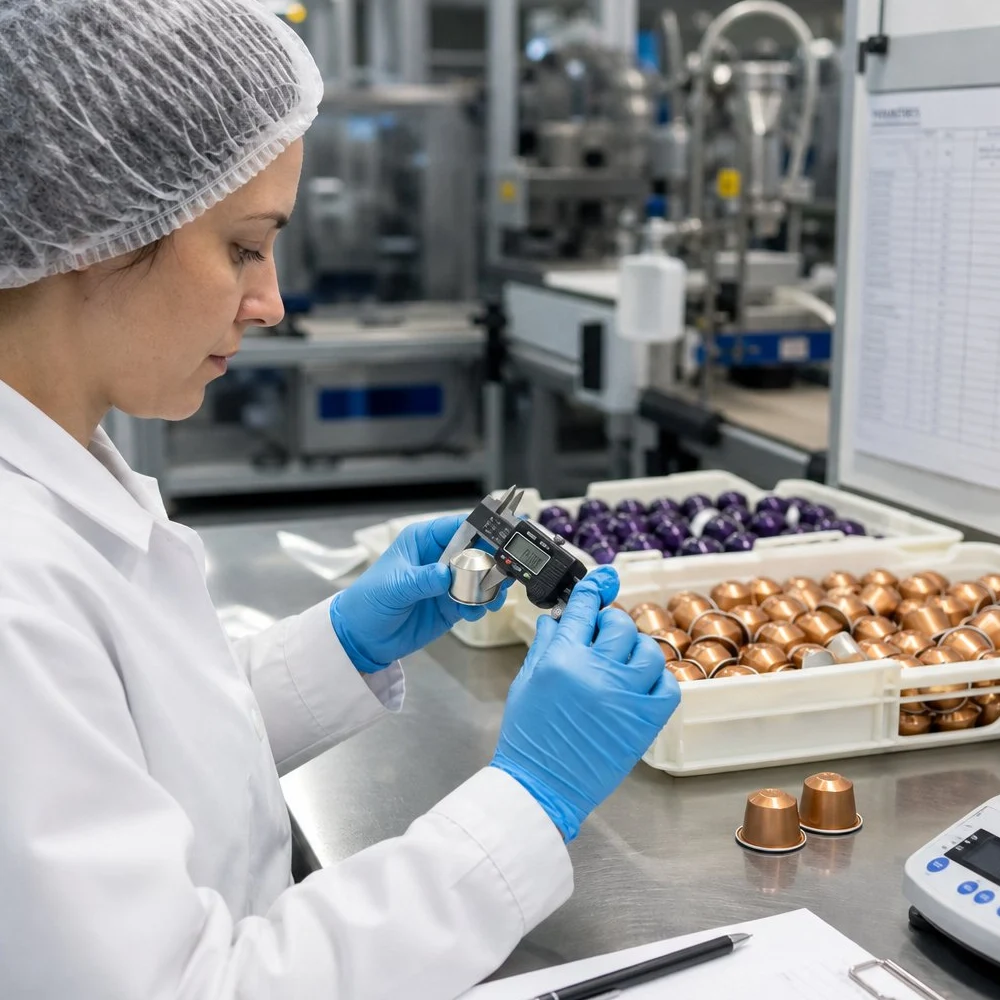
Total annual demand can be misleading when the business sells several products.
Suppose a company expects to use 240,000 capsules per year.
With one SKU, inventory planning is relatively straightforward.
Split the same annual demand across six colors or coffee variants and the situation changes.
Those SKUs probably won’t sell at identical rates.
One may account for 40% of volume. Another may represent only 5%. If purchasing is divided equally because it makes production simpler, slow-moving inventory starts to accumulate.
This is why the number of capsules isn’t the only unit worth planning.
Plan by SKU.
For each one, consider:
This becomes especially important with custom colors, printed capsules and branded packaging because the inventory may have little use outside that specific SKU.
An unprinted standard capsule is relatively flexible.
A capsule carrying a specific brand, color and product identity isn’t.
MOQ answers a specific question:
“What is the minimum quantity the supplier can reasonably accept for this production setup?”
It doesn’t answer:
“How much should my business buy?”
Those are different questions.
For standard products, lower order quantities may be possible because capsules are already available in inventory or can fit into an existing production plan.
Customization changes the economics. Dedicated colors, printing, lids or packaging may require production setup that makes very small runs inefficient.
At Kervoo, standard aluminum capsules can start from one carton of 4,000 pieces, subject to stock availability. For customized OEM projects, around 20,000 pieces per design is generally a more practical production starting point.
Those figures help define what’s available from the supply side.
Your demand still determines whether that quantity makes sense from the buying side.
For businesses deliberately testing a smaller market, low-MOQ empty aluminum coffee capsules can reduce initial inventory exposure. But once demand becomes predictable, repeatedly buying the smallest possible quantity may increase unit and logistics costs unnecessarily.
MOQ is a boundary.
It isn’t a forecast.
“50,000 capsules in stock” doesn’t tell you whether inventory is high or low.
At a consumption rate of 5,000 per month, that’s roughly ten months of inventory.
At 25,000 per month, it’s about two.
This is why purchasing teams often gain more insight by looking at inventory coverage rather than pieces alone.
A simple starting calculation is:
Couverture des stocks = stocks utilisables ÷ consommation moyenne par période
If you have 60,000 usable capsules and average consumption is 20,000 per month, that’s approximately three months of coverage.
Again, this isn’t a universal purchasing rule. It’s simply a way to make inventory easier to interpret.
Then adjust for reality.
Is next month’s demand unusually high?
Are some capsules reserved for confirmed production?
Is any inventory damaged or unavailable?
Do different SKUs have different consumption rates?
Once inventory is expressed as weeks or months of coverage, it becomes much easier to compare with supplier and shipping lead times.
That’s where reorder planning begins.
Buyers sometimes ask a supplier:
“What’s your lead time?”
Then they use that number as the replenishment period.
For international purchasing, that can be too optimistic.
The complete replenishment cycle may include:
Not every order experiences every delay, and some stages overlap.
The point is that “factory production time” and “time until inventory is usable in my warehouse” are not necessarily the same thing.
A practical reorder point therefore needs to account for expected demand during the full replenishment period, plus whatever safety stock the business decides is appropriate.
En résumé :
Seuil de réapprovisionnement = demande prévue pendant la période de réapprovisionnement + stock de sécurité
The formula is simple.
Choosing realistic inputs is the difficult part.
It would be convenient if every buyer could simply hold “20% safety stock” and stop thinking about it.
Real supply chains don’t work that neatly.
The appropriate buffer depends on how unpredictable demand is and how costly a stockout would be.
A mature product with stable monthly usage may require less relative protection than a rapidly growing SKU.
A product involved in seasonal promotions may need more.
An internationally sourced custom capsule with a long replenishment path carries a different risk from a standard product available locally.
Ask two questions:
How uncertain is our demand?
How uncertain is our replenishment?
Then consider what happens if either assumption is wrong.
If running out of one capsule SKU stops a filling line or prevents a retail order from being shipped, holding additional inventory may be cheaper than the stockout.
If the product is experimental and demand is uncertain, excess stock may be the larger risk.
Safety stock is therefore a risk decision.
Not a percentage copied from another company.
Unit price usually becomes more attractive as order volume increases.
Freight doesn’t always move in the same neat pattern.
A larger shipment may use transport space more efficiently, but the actual economics depend on carton configuration, palletization, destination, freight mode and current shipping conditions.
For lightweight products such as empty capsules, volume can matter as much as gross weight.
That’s why buyers should consider logistics while planning quantity—not after the purchase order is already fixed.
Questions worth confirming include:
How many capsules are packed per carton?
What are the carton dimensions and gross weight?
Will the shipment be palletized?
Is the order likely to move by courier, air or sea?
Does increasing quantity improve freight efficiency enough to justify the additional inventory?
At Kervoo, the standard packing quantity is 4,000 capsules per carton. Actual carton dimensions, pallet configuration and shipping method should be confirmed for the specific order.
For overseas buyers, coffee capsule packaging and international shipping should therefore be part of the purchasing calculation rather than a final administrative step.
As order sizes grow, purchasing mistakes become more expensive.
Forecasting doesn’t remove that risk, but it makes it more visible.
A useful forecast doesn’t need to predict the next twelve months exactly. A rolling forecast that updates regularly can often provide more value because it changes as real sales information becomes available.
For example, a buyer might track:
Next 1–2 months: relatively firm requirement
Months 3–4: expected requirement
Months 5–6: planning range
Again, those periods are examples, not a universal supply-chain standard.
The idea is to separate what you know from what you’re estimating.
Sharing some level of forward visibility with the supplier can also make stable coffee capsule supply easier to manage, particularly when custom colors, multiple SKUs or larger production quantities are involved.
The manufacturer gets time to plan.
The buyer gets more warning before stock becomes critical.
That’s a much healthier arrangement than every replenishment order beginning with:
“We need it urgently.”
One pattern appears repeatedly in bulk purchasing: buyers often spend more time negotiating the unit price than planning the next order.
The price is visible.
A future stockout isn’t.
Neither is slow-moving inventory sitting in a warehouse six months later.
After more than 10 years in aluminum coffee capsule manufacturing, we’ve found that the smoother repeat-order relationships tend to share something fairly simple: both sides have reasonable visibility.
The buyer understands roughly how quickly capsules are being consumed.
The manufacturer knows when demand is likely to increase.
SKU changes are discussed before the purchase order arrives.
Shipping isn’t left until the last minute.
None of this requires an elaborate supply-chain system.
It requires a few reasonably good numbers and regular communication.
For many buyers, that’s enough to make a much bigger difference than squeezing one more fraction out of the unit price.
If you’re preparing your next bulk capsule purchase, the planning sequence can stay fairly simple.
Start with expected consumption by SKU.
Subtract usable inventory already on hand or committed to arrive.
Estimate how much stock will be consumed during the full replenishment period.
Add the buffer your business considers appropriate.
Then check MOQ, production constraints, carton quantities and freight economics.
Only after that should quantity-based price breaks influence the final order.
En termes simples :
Planned requirement = demand until next replenishment
chosen safety stock − usable inventory available
Then adjust the result for MOQ, carton packing, SKU production constraints and logistics.
It’s not a perfect mathematical forecast.
It doesn’t need to be.
A reasonable plan based on real consumption and realistic lead times is usually more valuable than a very precise-looking order built around the wrong assumptions.
Foire aux questions
How many empty aluminum coffee capsules should I order in bulk?
There is no universal quantity. A practical order should consider expected consumption by SKU, current usable inventory, replenishment lead time, safety stock, MOQ, packaging and freight. Buying more simply to reach a lower unit price can create unnecessary inventory.
What is the MOQ for bulk aluminum coffee capsules?
MOQ depends on the product and customization. At Kervoo, standard capsules can start from one carton of 4,000 pieces when stock is available. Customized OEM projects generally become more practical from around 20,000 pieces per design.
Should I order all coffee capsule SKUs in equal quantities?
Usually not unless their demand is genuinely similar. Planning each SKU according to its expected consumption helps reduce slow-moving stock while protecting faster-selling products from shortages.
When should I place my next capsule order?
Ideally before inventory falls below the quantity needed to cover the complete replenishment period plus your chosen safety stock. International buyers should consider production, export preparation, transit, customs and local delivery—not factory production time alone.
Is a larger coffee capsule order always cheaper?
The unit manufacturing cost may improve at higher volumes, but total commercial cost can also include inventory carrying, packaging, freight and the risk of obsolete or slow-moving stock. Buyers should compare the total order economics rather than unit price alone.
Spécialiste de la fabrication de capsules de café · Kervoo
Depuis 2024
A buyer says they need private label coffee capsules. Another asks for OEM. A third uses both terms in the same email to describe exactly
A perfect sample is reassuring. It looks right. The color is right. It drops into the machine smoothly and brews without leaking. Put ten more

A Good Presentation Is Not the Same as Good Evidence. A supplier’s website, catalog and sales presentation are useful starting points. They can tell you